AirAccess Access Control as a Service Platform with Auto-Cell Networking (ACasS)
Enterprise Hosted Platform - MVPAccess™
New! Napco Access 1 & 2-Door Controllers
Please contact us directly or visit our FAQ page or Video Library.
Toll Free 800-645-9330
Phone 631-842-9400
Fax 631-842-9135
Email: sale@safehomeexpert.com
sale@safehomeexpert.com (Latin America)
Sign up for integrator training seminars. 2 days and 3 day online courses are available from our directory indexed by product.
Learn MoreOffer the one access control solution powerful and flexible enough to protect all of your clients. Continental Access provides state-of-the-art access control software and hardware in an easy-to-implement and easy-to-use access control solution that seamlessly integrate with a wide range of facility management products.
Learn MoreA Metal Sanding Machine is more than a motorized abrasive tool. It is a controlled system for removing scratches, scale, burrs, and uneven surfaces from metal. Its abrasive belt, disc, or wheel moves across the workpiece at a regulated speed. Pressure and contact time determine how much material disappears. The result can be a smooth finish, a uniform grain, or a surface prepared for coating and welding.
Dr. Ioan D. Marinescu, a widely cited researcher in grinding and abrasive processes, explains the core idea clearly: “Abrasive machining is controlled cutting, not merely rubbing.” That principle helps readers understand the machine’s action. Tiny abrasive grains cut metal fragments from the surface. They also generate heat, dust, vibration, and sometimes visible discoloration. These details matter. A machine may look simple, yet poor belt selection can leave deep lines or uneven edges. Excessive pressure can overheat thin stainless steel. The operator’s judgment remains important.
This guide examines the main components of a Metal Sanding Machine, including its drive motor, abrasive media, contact wheel, work table, and dust-control system. It also explains how the machine transfers force through the abrasive surface. Real workshop conditions are rarely perfect. Belts wear out. Metal thickness changes. Even experienced operators make mistakes. Understanding these limitations leads to safer settings and more consistent results. A clean finish begins with control, not speed alone.
A metal sanding machine is industrial equipment that removes burrs, rust, weld marks, and sharp edges from metal surfaces. It uses an abrasive belt, disc, drum, or brush instead of a cutting blade. The workpiece moves against the abrasive surface, while controlled friction gradually removes unwanted material. Operators can adjust belt speed, contact pressure, and feed rate for different metals.
Some machines process flat sheets. Others handle tubes, profiles, or welded frames. A wide-belt model can smooth a steel panel in one pass, leaving visible parallel finishing lines.
A smaller disc unit offers better control around corners and narrow edges. In practice, surface preparation is rarely perfectly uniform. Excess pressure may create grooves, heat discoloration, or premature abrasive wear.
Safety and dust control are essential parts of the machine’s design. OSHA sets the permissible exposure limit for respirable crystalline silica at 50 micrograms per cubic meter over an eight-hour shift, where silica-containing materials are involved. OSHA’s noise standard also uses an 85-decibel action level and a 90-decibel eight-hour permissible exposure limit. These figures explain why local extraction, hearing protection, guarding, and routine inspection matter.
According to industry abrasive-market reports, demand is closely linked to automotive, fabrication, construction, and machinery production. Yet productivity alone can mislead. A faster belt is not always better. Material hardness, abrasive grain, cooling, and operator experience must be matched carefully. Sometimes, a slower pass produces the more reliable finish.
A metal sanding machine removes scratches, burrs, and uneven edges with a coated abrasive belt or disc. Its motor drives the abrasive surface at a controlled speed. The operator guides the workpiece against it. Pressure must remain steady. Excess force can overheat the metal or wear the abrasive unevenly.
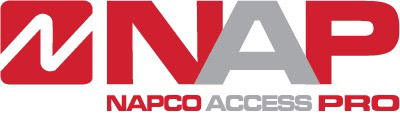
The abrasive belt does the cutting, while the platen supports it from behind. A contact wheel creates a rounded sanding area for tubes and curved edges. Flat tables support small parts and improve control.
Many machines include adjustable guides, which help maintain a consistent angle. I have found that even a small guide adjustment can change the finish noticeably.
The frame absorbs vibration during operation. A tensioning mechanism keeps the belt tight and centered. Without proper tension, the belt may wander or tear. The motor and speed control determine how aggressively the machine works.
Lower speeds suit delicate edges and heat-sensitive metals. A dust collection port captures particles near the sanding zone, although it cannot remove every airborne contaminant. The control panel usually includes start, stop, and emergency shutoff functions. Keep them within easy reach.
Gloves can catch near moving abrasives, so operators should follow the machine’s safety instructions carefully. Eye protection remains essential. I still inspect the belt, table, and cable before each use. That check takes little time. My early mistake was trusting a new belt too much; it still needed careful alignment.
A metal sanding machine removes burrs, oxidation, weld marks, and uneven edges with a rotating belt, disc, or abrasive wheel. Its motor transfers torque to the sanding surface. The operator guides the metal across it with controlled pressure. Abrasive grains then cut microscopic ridges from the workpiece.
The process starts with inspection. The operator checks thickness, welds, sharp edges, and surface contamination. The workpiece must stay firmly supported. A loose sheet can vibrate, catch, or distort. The operator selects an abrasive grade based on the required finish. Coarse grains remove heavy weld material; finer grains reduce visible scratches. Contact begins gradually. Pressure stays light and even. Excess force creates heat, loading, and uneven marks. That mistake is common.
Airflow removes part of the dust plume, while guards contain sparks and fragments. OSHA identifies 85 dBA as the action level for an eight-hour noise exposure, so hearing protection matters. The operator also checks dust controls and ventilation before production. Grand View Research valued the global abrasives market at about USD 47 billion in 2023, showing how widely abrasive processing is used. However, market size does not prove process quality. After each pass, the operator changes direction, checks the surface under angled light, and measures critical dimensions. The first setting may be wrong. A slower pass can sometimes produce a better finish with less heat.
| Step | Machine Function | Main Component | What Happens to the Metal | Typical Abrasive or Setting | Result and Quality Check |
|---|---|---|---|---|---|
| 1 | Loading and positioning | Worktable, conveyor, clamps, or feed rollers | The metal sheet, plate, tube, or fabricated part is placed on the machine and aligned with the sanding path. | Part-specific fixture; flat and stable support | Secure and aligned Confirm that the workpiece cannot shift during sanding. |
| 2 | Surface inspection | Operator controls and visual inspection area | Rust, mill scale, weld spatter, burrs, sharp edges, paint, or existing scratches are identified. | Inspection under adequate lighting; defect type determines the abrasive sequence | Process selected The machine setup is matched to the required surface condition. |
| 3 | Abrasive selection | Abrasive belt, disc, brush, or sanding head | The abrasive removes material through controlled contact between abrasive grains and the metal surface. | Coarse abrasives remove stock quickly; finer abrasives produce a smoother finish. Common grain types include aluminum oxide, zirconia alumina, and ceramic abrasive. | Correct removal rate The abrasive should remove the defect without excessive heat or gouging. |
| 4 | Machine adjustment | Drive motor, sanding head, pressure mechanism, and height control | The sanding head is set to the required height, contact pressure, and working position. | Pressure and depth are kept as low as practical while achieving the required finish; excessive pressure can cause heat and premature abrasive wear. | Controlled contact The abrasive contacts the workpiece evenly across the intended area. |
| 5 | Starting abrasive motion | Motor, drive rollers, spindle, or oscillating mechanism | The abrasive begins rotating, orbiting, oscillating, or moving continuously across the work surface. | Speed depends on abrasive type, workpiece material, contact area, and desired finish; the machine manual should determine operating limits. | Stable operation Check for unusual vibration, belt tracking problems, or abnormal noise. |
| 6 | Material removal | Abrasive contact zone | Abrasive grains cut and fracture small portions of the surface, removing burrs, scale, oxidation, weld marks, or uneven areas. | Use multiple passes or progressively finer abrasives when a uniform finish is required. | Defect reduced Inspect for remaining high spots, deep scratches, discoloration, and uneven material removal. |
| 7 | Dust and heat control | Dust-collection port, filter, guards, and optional coolant system | Generated dust and heat are controlled to improve visibility, protect the operator, and reduce the risk of surface overheating. | Dry sanding is common; liquid cooling may be used when compatible with the material and process. | Safe temperature The surface should not show heat tint, warping, burning, or other thermal damage. |
| 8 | Pass control and finishing | Feed system, speed control, and finishing abrasive | The part may pass through the machine once for aggressive removal or through several stages for blending and finishing. | Progress from coarse to fine abrasive grades when a smoother and more consistent finish is required. | Uniform appearance Check scratch direction, surface consistency, edge condition, and dimensional requirements. |
| 9 | Unloading and cleaning | Worktable, conveyor, air extraction, and cleaning tools | The finished part is removed, and loose abrasive particles and metal dust are cleared from the surface and work area. | Use suitable industrial vacuuming or approved cleaning methods; avoid unsafe handling of combustible metal dust. | Ready for inspection The part is clean, identifiable, and free from loose burrs or residue. |
| 10 | Final inspection and maintenance | Inspection tools, abrasive tracking system, guards, and filters | The finished surface is compared with the required specification, while the machine is checked for wear and buildup. | Inspection may include visual checks, surface-roughness measurement, dimensional checks, or edge-burr evaluation. | Process complete Replace worn abrasives, clean filters, inspect guards, and record any process adjustments. |
What Is a Metal Sanding Machine and How Does It Work?
Common Types of Metal Sanding Machines
Metal sanding machines remove burrs, weld discoloration, sharp edges, and surface marks with coated or bonded abrasives. A motor drives the abrasive belt, disc, drum, or brush. Controlled pressure then smooths the metal surface.
Belt sanders are common in fabrication shops. They handle flat bars, brackets, and welded frames efficiently. Narrow belts can reach corners, while wide-belt machines process sheets with more uniform pressure. Disc sanders suit short edges and small workpieces. The rotating disc gives operators strong control, but heat can build quickly.
Tube and pipe sanders use flexible belts around curved surfaces. They are useful for handrails, stainless-steel tubes, and finished cylindrical parts. Centerless sanding machines support continuous production. The workpiece moves between abrasive wheels without direct clamping. Drum and planetary systems offer broader contact for large panels.
A 2024 global abrasives market report estimated the sector at about 47.8 billion dollars in 2023. It also projected annual growth near 4.8 percent through 2030. That growth reflects demand for faster finishing and repeatable surface quality. However, sanding speed alone can mislead. Excessive pressure may leave blue heat marks, uneven edges, or hidden stress. In shop practice, technicians check grit condition, belt tracking, surface temperature, and final roughness after every adjustment. Small changes matter. Loose workholding remains a common weakness.
A metal sanding machine removes burrs, rust, weld marks, and uneven edges from metal surfaces. It usually uses an abrasive belt, disc, or wheel driven by a motor. As the abrasive moves across the workpiece, friction cuts away small amounts of material. Pressure and speed must remain controlled. Excessive force can overheat the metal, damage the abrasive, or create an uneven finish.
In workshops, these machines prepare steel panels, aluminum parts, welded frames, and fabricated components for painting or assembly. They can also smooth sharp edges before handling.
Operators should inspect the belt, guards, table, and electrical connections before starting. Secure the workpiece firmly, and keep both hands away from the abrasive path. Wear safety glasses, hearing protection, suitable work gloves when appropriate, and a fitted dust mask for airborne particles. Loose clothing and jewelry create avoidable risks. Never bypass a guard.
Tips: Begin with light contact and let the abrasive do the work. Keep the surface moving to prevent grooves and heat stains. Check the finish often, rather than removing too much material at once. Stop immediately if vibration, burning odor, or unusual noise appears.
Experienced operators still make mistakes when rushing, and a quick inspection may not reveal every problem. Follow the machine manual and workplace safety procedures for each material and operation.