AirAccess Access Control as a Service Platform with Auto-Cell Networking (ACasS)
Enterprise Hosted Platform - MVPAccess™
New! Napco Access 1 & 2-Door Controllers
Please contact us directly or visit our FAQ page or Video Library.
Toll Free 800-645-9330
Phone 631-842-9400
Fax 631-842-9135
Email: sale@safehomeexpert.com
sale@safehomeexpert.com (Latin America)
Sign up for integrator training seminars. 2 days and 3 day online courses are available from our directory indexed by product.
Learn MoreOffer the one access control solution powerful and flexible enough to protect all of your clients. Continental Access provides state-of-the-art access control software and hardware in an easy-to-implement and easy-to-use access control solution that seamlessly integrate with a wide range of facility management products.
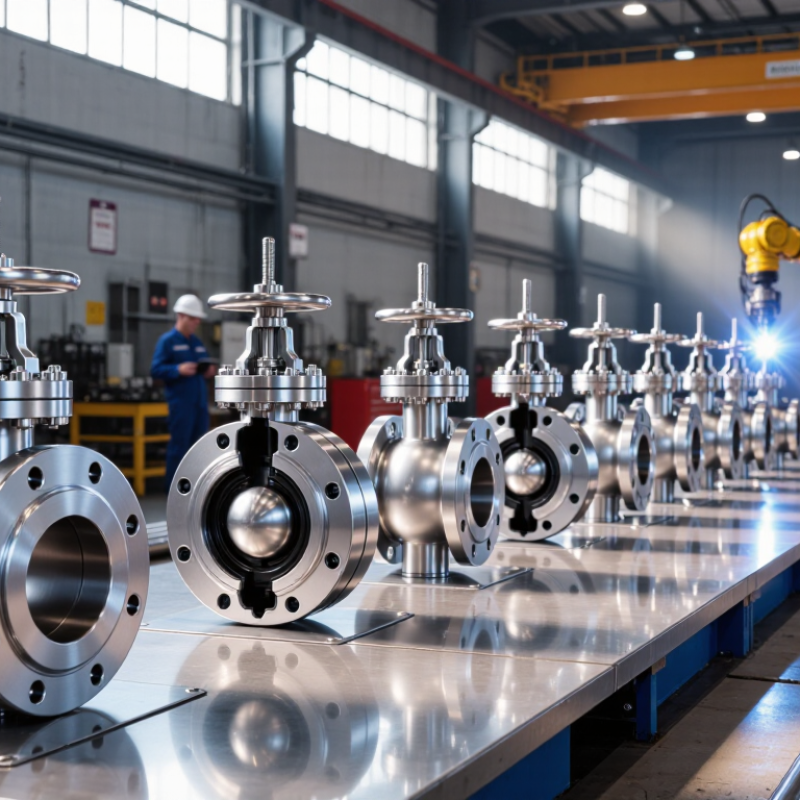
Learn MoreChoosing a Weld Ball Valve manufacturer is not simply a matter of comparing prices or brand names. In pipeline, processing, and utility systems, the right valve must suit the fluid, operating pressure, temperature range, and installation conditions. Welded connections can reduce potential leak paths, but they also make material selection, fit-up, and welding procedures especially important. Small details matter.
This guide reviews ten manufacturers worldwide and outlines practical points buyers can use when comparing them. It considers product range, material options, pressure ratings, manufacturing quality controls, documentation, and technical support. A useful supplier should provide clear specifications and traceability, not just polished catalog images. Buyers should also confirm that a valve’s design and test data match their project requirements; product descriptions alone are not enough.
There is no perfect list. Manufacturer capabilities, regional availability, and lead times can change, and a company’s reputation does not guarantee that every model fits every service. That deserves scrutiny. Before selecting a valve, compare the exact model, connection dimensions, materials, and inspection records. Ask how the supplier handles testing and after-sales questions. A datasheet is useful, but it cannot replace a careful technical review. The manufacturers below offer a starting point for research—not a substitute for project-specific engineering judgment.
A welded ball valve joins directly to a pipeline, usually through butt-weld ends. Inside, a bored ball turns a quarter turn: the bore aligns with the pipe to open flow, then rotates across it to shut flow. Seats press against the ball to limit leakage. Some designs use a full-size bore; others use a smaller one to reduce weight or cost. Simple movement. Strong sealing depends on careful sizing and installation.
Grand View Research estimated the global industrial valves market at about US$76.2 billion in 2023, with projected annual growth of 4.3% from 2024 to 2030. That figure covers many valve types, not welded ball valves alone, but it reflects broad demand across industrial piping. Welded ends remove bolted joints at the valve connection, which can reduce potential leak paths. The trade-off is harder removal: cutting the line may be necessary for service. A sound weld is not the whole story.
Tips: Match the valve material and pressure rating to the line, and check flow direction and operating temperature. Before welding, protect the seats and follow the valve maker’s procedure; heat can damage them. Inspect the finished joint. Even experienced teams can miss a small alignment problem.
A ball valve opens and closes by rotating its ball a quarter-turn. The chart shows representative ball positions; a 45° position does not necessarily provide 50% of the valve’s flow capacity.
A weld ball valve manufacturer should be evaluated against the actual service conditions, not just a polished catalog. Check the specified pressure, temperature, fluid, and pipe dimensions. Ask how the body and ball materials are selected, and request material traceability records. For welded ends, review documented welding procedures, welder qualifications, and inspection steps. Details matter. A small mismatch in end dimensions can complicate installation.
Tips: Request a sample inspection and recent pressure-test records. Ask what tests are performed, and how results are recorded. Confirm whether non-destructive examination is available when your project requires it. Compare the manufacturer’s stated limits with your operating conditions; do not assume a valve suitable for one line fits another.
Talk with the technical team about weld preparation, heat input controls, and post-weld inspection. Their answers should be specific and consistent with the documentation. Check lead times, spare-part support, and how design changes are communicated. Customer references can help, but they are not proof by themselves. I would also leave room for doubt: a neat certificate package cannot show every detail of production, so clarify what is verified on the actual valve before placing an order.
Choosing among the top 10 weld ball valve manufacturers worldwide means comparing more than price and pressure ratings. Check how each maker controls weld quality, verifies material traceability, and tests every valve before shipment. A well-documented process matters when a valve sits deep in a pipeline, where later access is difficult. Ask for pressure-test records and clear limits for temperature, pressure, and fluid compatibility.
MarketsandMarkets’ 2024 industrial valves market report estimated a global market value of USD 78.4 billion in 2024, with growth projected through 2029. This covers industrial valves broadly, not welded ball valves alone, so it should not be treated as a segment-specific forecast. For a practical supplier comparison, inspect the weld procedure, body material, seat design, and actuator options. Confirm that the quoted configuration suits the actual service conditions. A neat comparison table helps, but it can hide field headaches.
Tips: Request a sample inspection plan. Check weld documentation, test scope, and spare-part lead times. Small details matter. A polished datasheet is useful, but it cannot replace evidence from production and testing.
Leading welded ball valve manufacturers distinguish themselves through body design, weld-end accuracy, sealing systems, and documented testing. Full-bore models limit pressure loss, while reduced-bore designs can save space and weight. Compare body materials, pressure ratings, temperature ranges, and actuation options. Weld preparation matters.
Grand View Research’s 2024 Industrial Valves Market report valued the broad market at USD 78.42 billion in 2023 and forecast 4.4% annual growth through 2030. This figure covers many valve types, not welded ball valves alone. Leading suppliers commonly offer forged or cast bodies, fire-safe designs, anti-static features, and options for demanding temperatures. Look for traceable materials and clear inspection records, not just a long product list. Published test details can still be hard to compare.
Tips: Request material certificates, qualified welding procedures, non-destructive examination records, and hydrostatic and seat-leakage results. For actuated valves, check torque data. Fit matters. Confirm end dimensions before procurement; small mismatches can complicate installation. A polished brochure is not proof.
Choosing among weld ball valve manufacturers starts with the service, not the catalog. Define the media, pressure, temperature, cycling frequency, and exposure to thermal shock. A valve handling clean water may not suit abrasive slurry or corrosive condensate. Be specific. Compare body and trim materials against process chemistry, then check pressure-temperature ratings and documented test methods. Ask whether weld-end dimensions match site piping and whether the supplier provides heat-input guidance, purge instructions, and post-weld inspection requirements. Small details matter.
Look beyond headline capacity. Review quality records, material traceability, qualified welding procedures, inspection plans, and hydrostatic and seat-leakage reports. Confirm the acceptance criteria, not just whether a valve was “tested.” Ask how seats and seals perform after repeated cycles, and whether torque data supports the planned actuator. For critical lines, request references for comparable service, plus spare-part lead times and repair instructions. A responsive technical team can clarify trade-offs before purchase.
A neat datasheet is not proof of field suitability. Compare equivalent sizes, pressure classes, materials, and test conditions; otherwise, prices and claims can mislead. No checklist captures every installation. I would pause over missing evidence, even when delivery is urgent, and ask for deviations to be explained in writing. Also consider access for welding, inspection, and future removal. A sound valve can still be awkward to maintain.
Comparison framework for assessing ten supplier candidates. The entries below are anonymized supplier archetypes, not named companies, a verified ranking, or claims about specific manufacturers. Capability ranges are indicative of commonly specified industrial offerings; confirm the exact design, materials, ratings, certificates, and test documentation for each quoted valve.
| Supplier profile | Typical application focus | Welded-end and size considerations | Pressure and design references to check | Materials to evaluate | Quality and qualification evidence to request |
|---|---|---|---|---|---|
| 01 · Pipeline service | Onshore or offshore transmission and process pipelines | Butt-weld ends; confirm pipe schedule, end preparation, and bore matching. Size range is model-dependent. | Check the specified ASME pressure class and whether the design is suitable for the pipeline code and service conditions; API 6D may be relevant. | Carbon steel or low-temperature carbon steel; confirm trim and seat compatibility with the fluid. | Request design documentation, pressure-test records, material traceability, and applicable API 6D evidence. |
| 02 · High-pressure process service | Refineries, chemical plants, and high-pressure process lines | Welded ends can reduce flange joints; verify wall thickness, welding procedure requirements, and installation access. | ASME B16.34 and applicable ASME pressure classes, such as Class 300–2500, may be relevant; confirm the specific pressure-temperature rating. | Carbon steel, alloy steel, or stainless steel, selected for pressure, temperature, and corrosion conditions. | Review pressure-temperature tables, design calculations, inspection records, and pressure tests to the specified standard. |
| 03 · Corrosive chemical service | Chemical processing and corrosive liquid or gas duties | Confirm weld-end dimensions and whether the valve’s internal surfaces and seats suit the process fluid. | Specify the governing design and test standards; pressure class alone does not establish chemical compatibility. | Stainless steel or other corrosion-resistant alloys where justified; verify wetted-part materials against the process chemistry. | Request material certificates, wetted-parts list, corrosion compatibility confirmation, and test documentation. |
| 04 · Low-temperature service | Refrigeration, low-temperature processing, and cryogenic applications | Check extended bonnet or other required configuration, end dimensions, and installation orientation. | Confirm design temperature limits, pressure-temperature ratings, and any required low-temperature testing. | Low-temperature-qualified carbon steel or stainless steel, as appropriate to the minimum design temperature. | Request impact-test records where specified, material traceability, and documented low-temperature qualification. |
| 05 · High-temperature service | Steam, hot oil, and elevated-temperature process lines | Verify thermal expansion allowances, end preparation, and the specified pipe schedule. | Check the pressure-temperature rating at operating temperature and the applicable design standard. | Temperature-appropriate carbon or alloy steel; confirm seat, seal, and stem materials for the full temperature range. | Request temperature limits for all pressure-containing and sealing components, plus inspection and pressure-test records. |
| 06 · Gas and fugitive-emissions service | Gas processing and services with defined external-emissions requirements | Confirm stem-sealing design, welded-end details, and compatibility with the line’s operating conditions. | Specify the required emissions qualification; ISO 15848 is a relevant reference when required by the project. | Materials should be selected for the gas composition, pressure, temperature, and decompression conditions. | Request the applicable emissions test report and clarify its tested configuration, conditions, and qualification scope. |
| 07 · Fire-safe process service | Hydrocarbon processing and installations with fire-safe valve requirements | Check that the offered welded-end model—not only a related model—has the required qualification. | API 607 or API 6FA may be specified, depending on the valve and project requirements. | Confirm body, seat, and secondary sealing materials for both normal operation and the specified fire-test requirements. | Request a fire-test certificate or report identifying the tested design and applicable size and pressure range. |
| 08 · Utility and general industrial service | Water, air, and general plant utility systems | Match bore and weld ends to the piping specification; verify the required face-to-face or end-to-end dimensions. | Define the required pressure class, operating temperature, and project test standard before comparing quotations. | Common options include carbon steel and stainless steel, subject to fluid quality and corrosion requirements. | Compare dimensional drawings, material records, pressure-test documentation, and stated inspection scope. |
| 09 · Severe-service or specialized duty | Applications involving demanding pressure, temperature, cycling, or process conditions | Assess valve geometry, flow requirements, actuator interface, weld access, and maintenance strategy. | Use the project’s specified design code and operating envelope; confirm limits for the exact valve configuration. | Specify body, trim, seat, and seal materials from the process conditions rather than from a generic material list. | Request application references, engineering review, inspection plan, and qualification evidence relevant to the duty. |
| 10 · Project and custom-engineered supply | Large projects with project-specific documentation, traceability, or configuration needs | Confirm drawing approval process, weld-end tolerances, pipe schedule, and any project-specific dimensional requirements. | List all applicable design, testing, and project standards in the purchase specification; avoid relying on a generic class label. | Document approved materials for pressure boundary, trim, seats, and seals, including any project-specific restrictions. | Evaluate document index, inspection and test plan, material traceability, nonconformance process, and delivery documentation. |