AirAccess Access Control as a Service Platform with Auto-Cell Networking (ACasS)
Enterprise Hosted Platform - MVPAccess™
New! Napco Access 1 & 2-Door Controllers
Please contact us directly or visit our FAQ page or Video Library.
Toll Free 800-645-9330
Phone 631-842-9400
Fax 631-842-9135
Email: sale@safehomeexpert.com
sale@safehomeexpert.com (Latin America)
Sign up for integrator training seminars. 2 days and 3 day online courses are available from our directory indexed by product.
Learn MoreOffer the one access control solution powerful and flexible enough to protect all of your clients. Continental Access provides state-of-the-art access control software and hardware in an easy-to-implement and easy-to-use access control solution that seamlessly integrate with a wide range of facility management products.
Learn MoreThe 2026 Top Chromium Carbide Overlay Plate Manufacturers guide examines suppliers shaping wear protection across mining, cement, recycling, and bulk-material handling. Chromium Carbide Overlay Plate combines a tough steel backing with a hard, carbide-rich surface. This structure helps resist abrasion from crushed rock, clinker, coal, and mineral concentrates.
Selection requires more than comparing prices. Buyers should examine carbide distribution, crack patterns, overlay thickness, welding consistency, and dimensional accuracy. A plate may look impressive under warehouse lighting, yet fail quickly beside a vibrating transfer chute. Service temperature, impact frequency, material size, and installation method also influence real performance.
Dr. John C. Lippold, a respected welding-metallurgy specialist, has stated: “Weld performance depends on metallurgy and service conditions.” That principle deserves attention here. Manufacturer claims should be checked against test reports, traceable chemistry, production experience, and customer references. Independent verification is valuable.
This guide compares leading manufacturers through those practical criteria. It considers manufacturing capacity, quality control, customization, technical support, and delivery reliability. It also recognizes an uncomfortable limitation: no ranking can fit every application. A plate optimized for fine abrasive dust may perform poorly under heavy impact. Mistakes happen when catalog hardness replaces engineering judgment.
Readers should treat this overview as a starting point, not a final purchase decision. Ask for application-specific data. Inspect the details. That is where durability is usually won.
Chromium carbide overlay plates are wear-resistant steel plates with a hard alloy layer metallurgically bonded to a mild steel or low-alloy steel base. The overlay usually contains chromium-rich carbides within a tougher metallic matrix. These carbides resist sliding abrasion, impact from mineral particles, and erosion from abrasive mixtures.
The base plate provides structural support. The overlay provides surface protection. This combination suits chutes, hoppers, liners, screens, and transfer points exposed to coal, cement, stone, or metallic ore.
Hardness can vary widely, often depending on carbon content, chromium level, welding process, and cooling conditions. Higher hardness does not always mean better service. Excessive hardness may reduce impact tolerance and complicate cutting or installation.
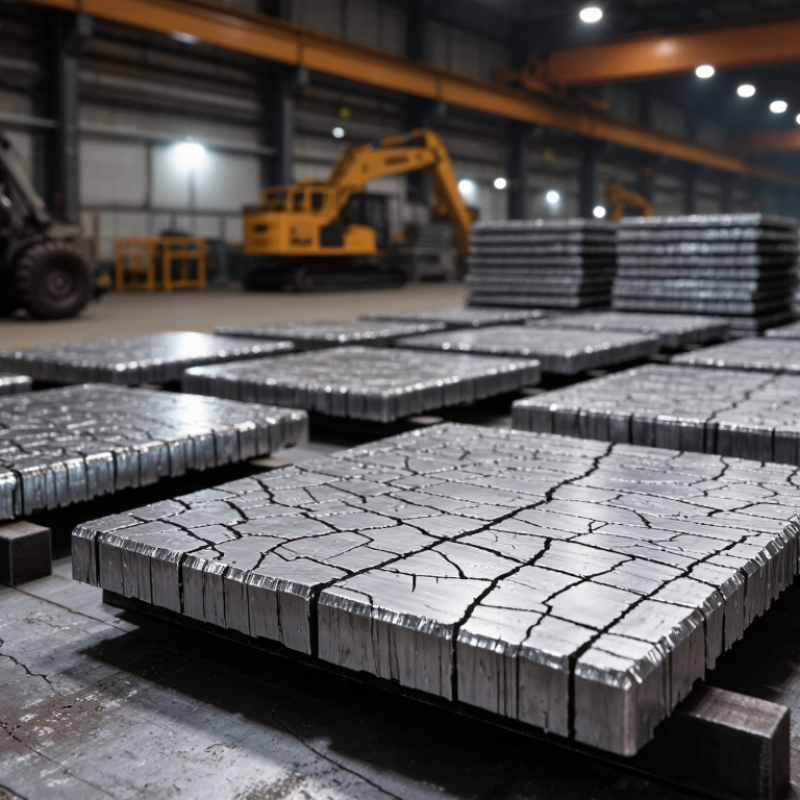
Plate thickness and overlay uniformity require close inspection. Practical checks include surface crack patterns, hardness mapping, chemical analysis, and ultrasonic bonding tests. Fine transverse cracks can relieve welding stress and may be acceptable. Large cracks, poor bonding, or uneven deposits are different concerns. They need investigation.
In abrasive slurry systems, edges often wear faster than flat surfaces. That detail is easy to miss. Designers should consider flow direction, impact angle, fastening methods, and replacement access. Overlay plates are not indestructible. Incorrect support, excessive heat during cutting, or weak joints can shorten their service life. The term “wear-proof” is misleading and deserves careful review.
Manufacturing chromium carbide overlay plate begins with selecting a tough carbon steel base. Its thickness depends on the intended wear conditions. Experienced fabricators inspect the plate for dents, scale, and surface contamination. The steel is then blasted and preheated when necessary. Clean steel matters.
A flux-cored welding system deposits an alloy-rich layer across the working surface. The welding wire contains chromium, carbon, and iron-based materials. As the arc travels, bright beads build a hard, carbide-forming matrix. Operators control current, travel speed, overlap, and interpass temperature. Excess heat can create distortion or excessive dilution. Both reduce service performance. Manufacturers often apply one or more passes, depending on the required thickness. The overlay may look uniform, yet cooling can leave small variations.
After welding, technicians measure thickness at several points. They also check bead appearance, bonding, and surface cracking. Hardness testing helps confirm the expected wear resistance. Ultrasonic examination may reveal weak bonding beneath the visible layer. The plate is then cut to size using controlled thermal or abrasive methods. Waterjet cutting can reduce heat influence near the edges. Edges still need careful grinding.
In my experience, production records are as important as test results. They connect welding settings with each finished plate. A perfect-looking surface does not guarantee perfect internal quality. That is worth remembering. Reliable manufacturing requires inspection, process discipline, and honest reporting when results vary.
| Manufacturing / Evaluation Dimension | Typical Industrial Practice | Common Technical Range or Requirement | Why It Matters |
|---|---|---|---|
| Base Plate Material | Low-carbon or mild steel plate is commonly used as the structural backing. | Typical carbon steel backing thickness: approximately 3–25 mm, depending on application. | Provides load-bearing strength, weldability, and support for the wear-resistant overlay. |
| Overlay Alloy System | Iron-based weld metal containing chromium carbides, with carbon and chromium as the principal alloying elements. | Chromium content is often about 15–35%; carbon is commonly about 2–6%, depending on formulation. | Controls carbide formation, abrasion resistance, crack pattern, and weld-metal toughness. |
| Surface Preparation | The backing plate is cleaned by removing oil, rust, moisture, scale, and loose contaminants before welding. | A clean, dry, metallic surface is required in the weld zone. | Reduces porosity, lack of fusion, inclusions, and premature delamination. |
| Overlay Deposition Process | Open-arc, submerged-arc, flux-cored arc, or other controlled welding processes may be used according to plate design. | The process is selected for deposition rate, plate size, alloy chemistry, and required surface profile. | Determines productivity, dilution, bead quality, heat input, and consistency across the plate. |
| Preheating and Interpass Control | Temperature is controlled to limit thermal shock and manage hydrogen-related cracking in the backing steel. | The required temperature depends on base-steel chemistry, thickness, restraint, and welding consumables. | Supports weld integrity and helps control distortion and cracking. |
| Overlay Thickness | One or more weld layers are deposited to achieve the required wear allowance. | Common finished overlay thickness: approximately 3–15 mm; heavier designs may exceed this range. | Greater thickness generally provides more wear allowance, but may increase weight and residual stress. |
| Carbide Microstructure | Primary chromium-rich carbides form within an iron-based eutectic matrix during solidification. | Typical carbide volume fraction is approximately 20–40%, depending on alloy and deposition parameters. | Carbide size, distribution, orientation, and matrix chemistry strongly affect abrasive wear performance. |
| Hardness Measurement | Hardness is tested on the overlay surface using a suitable standardized method. | Typical overlay hardness is about 55–65 HRC, or approximately 600–800 HV, subject to alloy and test location. | Confirms whether the deposited layer meets the specified resistance to abrasive wear. |
| Surface Crack Pattern | Fine transverse stress-relief cracks may appear in chromium carbide overlay weld metal. | Crack spacing commonly falls in the range of roughly ger 20–100 mm, but it varies with alloy, thickness, and heat input. | Controlled surface checking can relieve welding stress; unacceptable cracks or cracks reaching the backing plate require evaluation. |
| Dimensional Tolerance | Plates are inspected for length, width, total thickness, flatness, and overlay uniformity. | Tolerance is normally agreed in the purchase specification; cutting and forming allowances must be defined before production. | Ensures the plate can be fitted, formed, welded, or bolted into the intended equipment. |
| Cutting and Fabrication | Plates may be cut using plasma, abrasive, or other suitable methods; cutting is normally performed from the backing side when practical. | Machining of the hard overlay is limited; grinding or specialized cutting tools may be required. | Correct fabrication methods protect the overlay and reduce heat-affected damage. |
| Quality Inspection | Inspection may include visual examination, dimensional checks, hardness testing, chemical analysis, and ultrasonic or other nondestructive testing when specified. | Inspection scope should be agreed before order placement and recorded on the inspection certificate. | Verifies overlay continuity, bonding quality, chemistry, dimensions, and traceability. |
| Typical Applications | Mining, cement, steel, power generation, aggregate processing, recycling, and bulk-material handling equipment. | Suitable for sliding, gouging, or low-to-moderate impact abrasion; severe impact may require a different alloy system. | Application conditions determine whether chromium carbide overlay is the appropriate wear solution. |
| Selection Criteria for 2026 Purchasing | Evaluate alloy chemistry, overlay thickness, backing grade, production process, inspection capability, fabrication support, and delivery capacity. | Use application-specific requirements rather than hardness alone when comparing manufacturers. | A balanced specification improves service life, installation reliability, and total operating cost. |
Note: Technical ranges are representative industry values. Actual chemistry, hardness, dimensions, crack spacing, inspection methods, and tolerances vary by overlay formulation, welding procedure, backing material, and purchaser specification.
Ranking top chromium carbide overlay plate manufacturers in 2026 requires evidence beyond polished catalogs. Real field experience matters. Buyers should examine plates used in chutes, hoppers, crushers, and cement transfer lines. Ask for service records, not broad promises. Photographs can show uneven weld beads, edge cracking, or premature wear. These details often reveal production discipline.
Technical scoring should cover chemistry, overlay hardness, base-plate toughness, thickness tolerance, and weld quality. A credible manufacturer provides batch-level test reports and heat numbers. Independent laboratory verification adds weight when claims seem unusually precise. Test methods must reflect actual duty, since sliding abrasion differs from repeated impact. Compare cut edges, bend behavior, and dilution after welding. Harder is not always better. That point is easy to miss.
Reliability includes delivery consistency, technical support, and transparent correction procedures. Evaluate how a supplier handles a failed sample or disputed measurement. Fast answers are useful, but documented answers are stronger. Look for trained application engineers who can recommend overlay orientation, welding consumables, and allowable heat input. Certifications support confidence, yet certificates alone cannot prove plate life. A small pilot installation can expose assumptions before a full shutdown. My own ranking would reserve points for honest limitations, because no plate suits every abrasive environment. Manufacturers should state uncertainty, including expected wear ranges and inspection intervals.
Leading Chromium Carbide Overlay Plate Manufacturers to Consider
Choosing a chromium carbide overlay plate manufacturer requires more than comparing prices. Published reports support this caution. Grand View Research estimates the global wear-resistant steel market will expand steadily through 2030, driven by mining, cement, recycling, and bulk-material handling. Demand is rising, but quality varies sharply between suppliers.
Consider manufacturers with controlled welding procedures, documented carbide chemistry, and repeatable overlay thickness. Ask for mill certificates, hardness results, bend-test records, and dimensional inspection data. A serious producer should explain carbide distribution, matrix composition, dilution, and heat-affected zones in plain language. They should also provide samples from the same production route, not only laboratory photographs.
Small details matter.
During plant inspections, uneven bead spacing often signals inconsistent heat input. Excessive surface cracking may be acceptable in some grades, but it should never be dismissed without application guidance. Manufacturers serving chutes, liners, crushers, and high-impact zones should recommend different microstructures for each duty. ASTM and ISO-based quality systems add confidence, although certification alone cannot replace traceability.
MarketsandMarkets and other industry studies identify mining and construction as major wear-material users, reflecting the cost of unplanned shutdowns. Still, market forecasts are not purchase specifications. I would compare tested service data, repair support, and lead times before approving a supplier. A cheaper plate can become expensive when drilling, fitting, or replacement work fails. That risk is easy to underestimate.
Typical technical benchmarks used when evaluating chromium carbide overlay plate suppliers. The values represent midpoints of commonly published industry ranges and are not company-specific data.
Chromium carbide overlay plates commonly feature approximately 20–30% chromium, 4–5% carbon, 55–65 HRC overlay hardness, and a 3–40 mm total plate thickness range. Actual specifications vary by welding process, substrate, and application.
Chromium carbide overlay plates protect equipment exposed to severe sliding abrasion and moderate impact. Common applications include mining chutes, crusher liners, cement conveyors, hoppers, and steel transfer systems. In practice, wear patterns matter more than industry labels. A chute carrying sharp quartz behaves differently from one handling damp coal.
Performance depends on carbide distribution, overlay thickness, base plate strength, and welding quality. Harder is not always better. Excessive hardness can reduce impact resistance and increase cracking around stressed bends. Surface checking may be normal, but open cracks require inspection. Operating temperature, particle size, impact angle, and material moisture also influence service life. Small details matter.
Buyers should request chemistry data, hardness ranges, thickness tolerances, and production traceability. Ask how the plate was tested, not only for a polished certificate. Cut samples can reveal uneven layers or excessive dilution. Measure the existing liner before ordering; drawings are sometimes outdated. Consider installation time, hole placement, bending limits, and repair access. A thicker plate may last longer, but it can reduce chute capacity and add structural load. Field feedback should be recorded honestly, including failed trials. That uncomfortable information often improves the next selection.